Description: The company manufactures a full range of industrial reducers and motorized pulleys. Complete specifications and abundant models are available to adapt to various industrial transmission scenarios. We also undertake custom processing of non-standard special-shaped reducers and gear equipment to meet enterprises' transmission supporting requirements.
Release Time: 2026-10-30
Views: 2
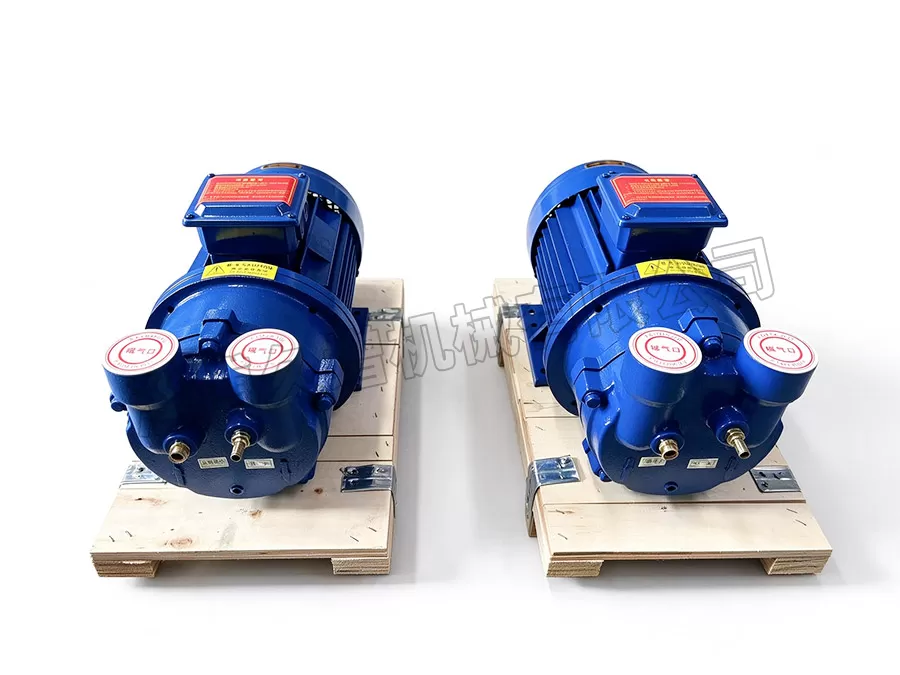
The 2BV series liquid ring vacuum pump is a single-stage pump with an integrated coaxial structure of pump and motor. It adopts a mechanical shaft seal, featuring simple structure, quick installation and oil-free operation.
The 2BV series liquid ring vacuum pump is suitable for extracting gases and moist vapors. Its inlet pressure can reach an absolute pressure of 33 mbar (97% vacuum). If the 2BV liquid ring vacuum pump operates continuously at an inlet pressure below 80 mbar, a cavitation protection pipe shall be connected for pump protection. When equipped with an atmospheric ejector, the inlet pressure of the pump can be as low as 10 mbar, and the ejector can be mounted directly on the suction port of the vacuum pump. When used as a compressor, its maximum pressure reaches 0.26 MPa (absolute pressure).
2BV series liquid ring vacuum pumps and compressors are widely used in petroleum, chemical, pharmaceutical, food, sugar-making and other industries. Since gas compression is isothermal during operation, the risk of explosion is low when compressing and pumping flammable and explosive gases, which further broadens its application scope.